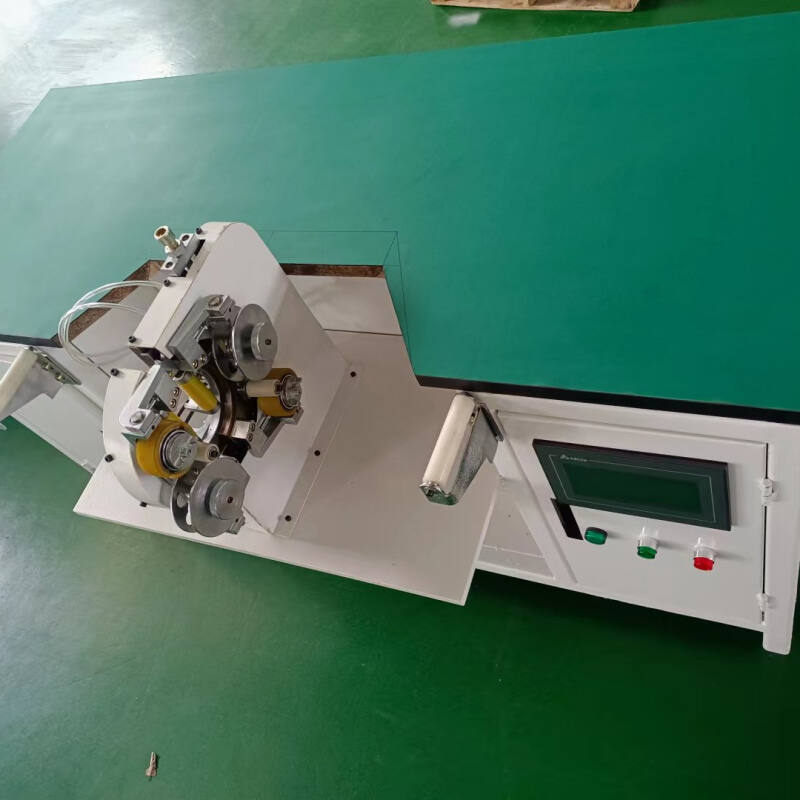
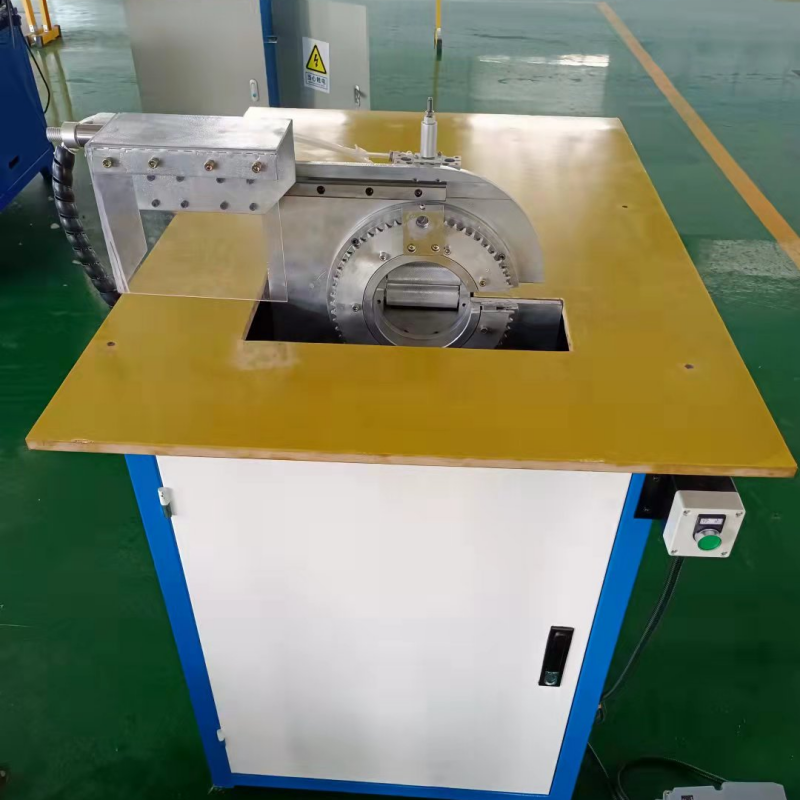
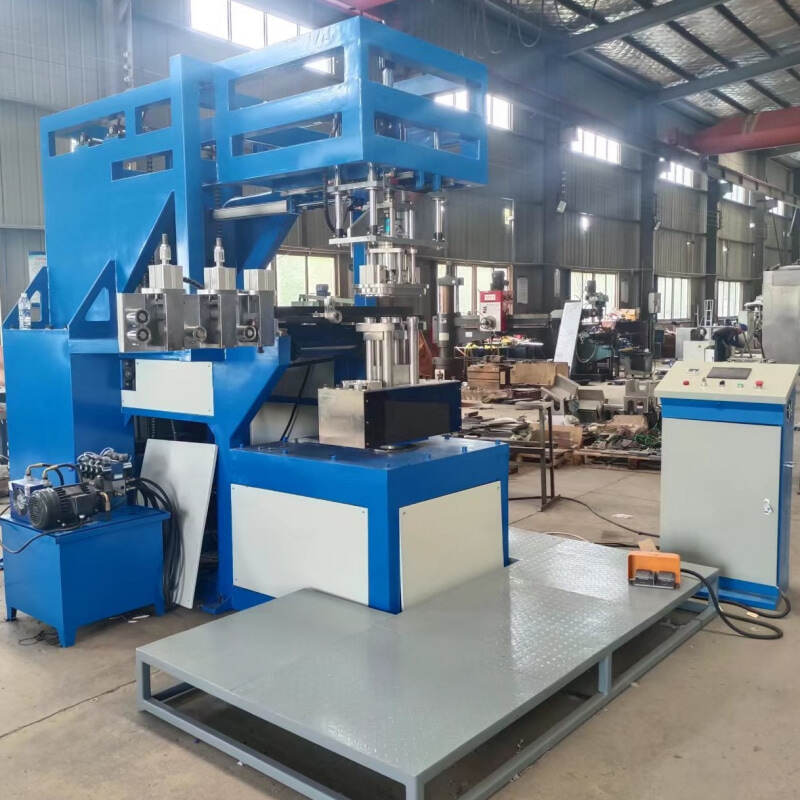
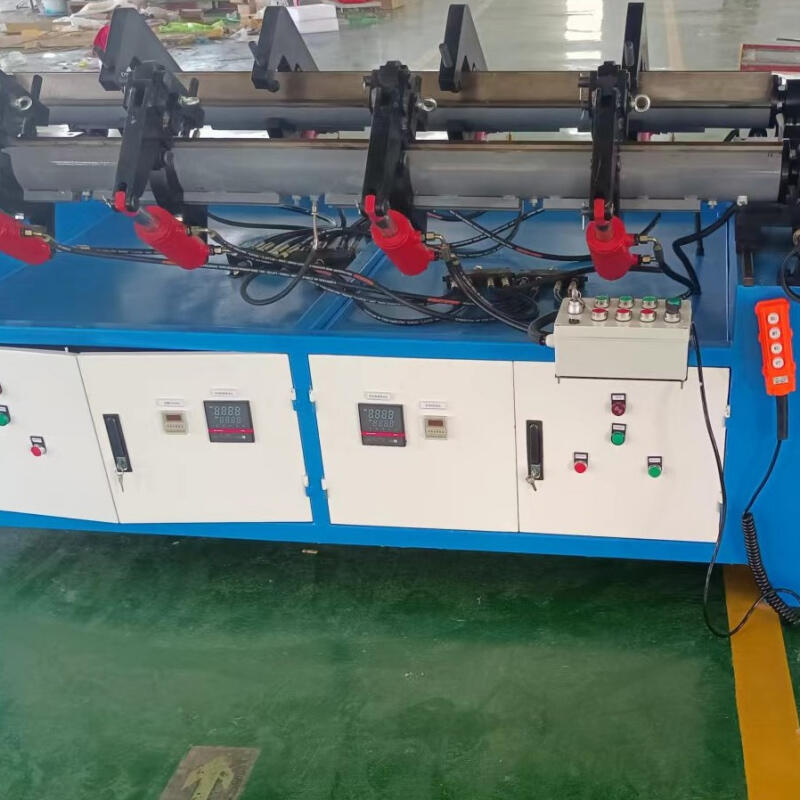
new automatic packaging machine
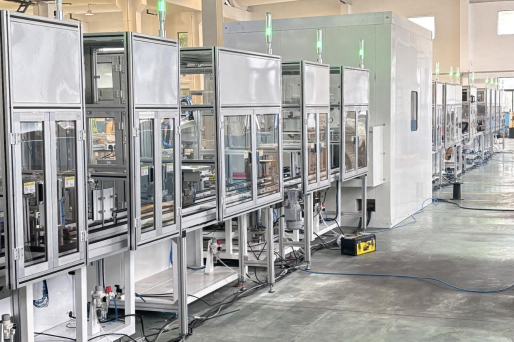
The new automatic packaging machine represents a significant advancement in modern packaging technology, designed to streamline production processes across diverse industries. This innovative equipment integrates cutting-edge automation systems with precision engineering to deliver consistent, high-quality packaging results. At its core, the new automatic packaging machine combines multiple functions including product feeding, measuring, filling, sealing, labeling, and quality inspection within a single integrated platform. The machine utilizes advanced servo motor technology and programmable logic controllers to ensure accurate operation at various production speeds. Its modular design allows manufacturers to customize configurations based on specific product requirements, whether packaging powders, liquids, granules, or solid items. The technological features of this new automatic packaging machine include touchscreen interface controls that simplify operation and reduce training time for workers. Real-time monitoring systems track production metrics, material consumption, and machine performance, enabling managers to make data-driven decisions. The equipment incorporates automatic error detection mechanisms that minimize waste by identifying and rejecting defective packages before they reach the final stage. Energy-efficient components reduce operational costs while maintaining optimal performance levels throughout extended production runs. Applications for the new automatic packaging machine span numerous sectors including food and beverage, pharmaceuticals, cosmetics, chemicals, agriculture, and consumer goods manufacturing. Food processors use these machines to package snacks, coffee, spices, and frozen products with consistent weight accuracy and hermetic sealing. Pharmaceutical companies rely on the sterile packaging capabilities to ensure product safety and compliance with regulatory standards. The versatility of the new automatic packaging machine makes it suitable for both small-scale operations seeking to increase efficiency and large manufacturers requiring high-volume output. Its compact footprint optimizes floor space utilization while delivering production capacity that rivals much larger systems, making it an ideal solution for facilities with space constraints or growth ambitions.
 ×


 EN